Learn & FAQ
Waterjet cutting, explained
Waterjet cutting is a versatile and efficient method for highly accurate cutting of a wide range of materials. Below you will find more information and frequently asked questions to help you understand the benefits, applications and technologies of waterjet cutting. Discover an environmentally friendly and precise cutting method that can improve manufacturing processes and increase productivity.
Waterjet cutting in general
How does waterjet cutting work?
A waterjet cutter, also known as a waterjet cutting machine or waterjet system, is an industrial cutting machine capable of cutting almost all materials in practically any shape. It is a non-thermal cutting method based on the extremely high speed of the waterjet and the energy it creates.
Water pressure is increased to a very high level using a high-pressure pump. Pressures of up to 6200 bar can be achieved. This pressurised water is directed as a waterjet onto the material placed on the cutting table. Through erosion, the waterjet removes material efficiently and accurately, separating the cut parts from the sheet or workpiece.
There are two main types of waterjet cutting: cutting with water only, known as pure waterjet cutting, and cutting with a mixture of water and abrasive, known as abrasive waterjet cutting.
Both methods are commonly referred to as waterjet cutting.
Comparison
Pure waterjet
Pure waterjet cutting is typically used for softer materials such as plywood, plastics or rubber.
Abrasive waterjet
Adding abrasive sand to the waterjet increases the cutting energy and makes it possible to cut hard materials such as metals, stone, glass or carbon fibre.
Benefits
What are the benefits of waterjet cutting
Waterjet cutting is a versatile and efficient method for highly accurate cutting of a wide range of materials. Below you will find some frequently asked questions that help explain the benefits, applications and technologies of waterjet cutting. Discover an environmentally friendly and precise cutting method that can improve manufacturing processes and increase productivity. Waterjet cutting offers several advantages that make it an excellent choice for many different industries. This versatile cutting method can process a wide range of materials, from metals and ceramics to composites and glass, while offering excellent accuracy and efficiency.
Waterjet cutting combines accuracy, efficiency and environmental friendliness. Discover how Muototerä’s FinJet waterjet cutting machines can improve your manufacturing processes and increase productivity. For more information or personal advice, please contact our team.
Versatility
No limits
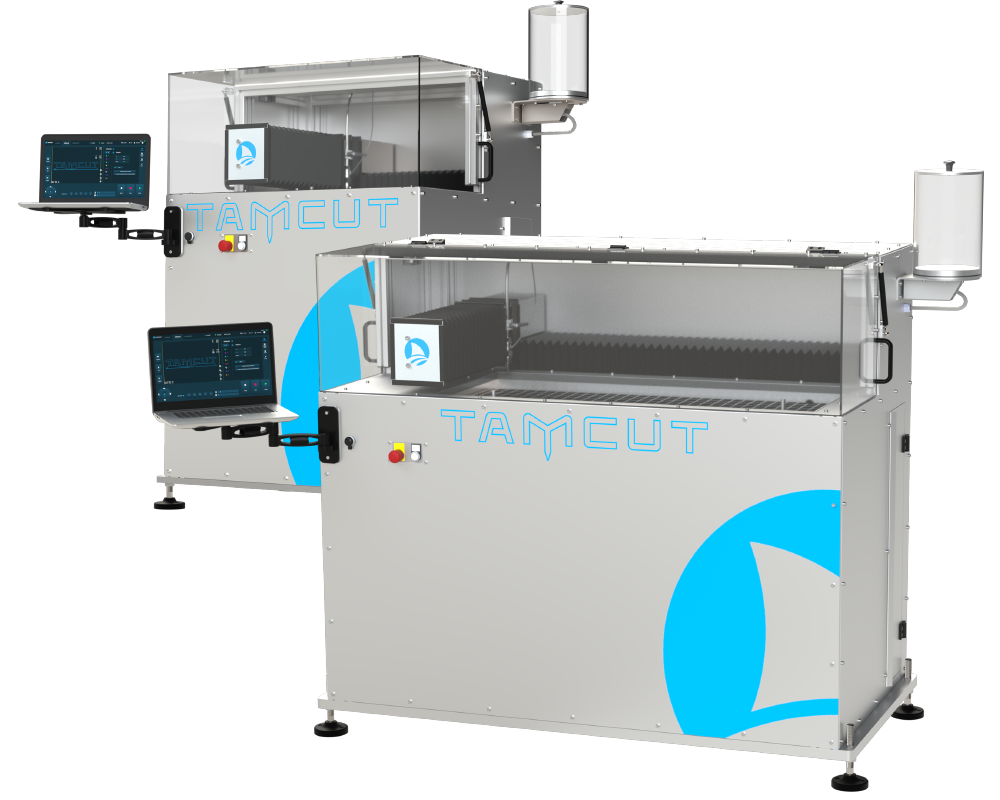
In practice, waterjet cutting has very few material limitations. Almost all materials are suitable for waterjet cutting, and both very thin materials, below 1 mm, and very thick materials, over 350 mm, can be cut with waterjet technology. TamCut provides cutting capability up to 30-50 mm, depending on the material.
Common cutting materials include metals, rubber, stone, glass, plywood, plastics, foams, textiles, food products, leather and many others. This makes waterjet cutting ideal for a wide range of industries, including aerospace, automotive, mechanical engineering, shipbuilding, construction, food industry and many more.
Quality
Meets your expectations
Waterjet cutting does not create a heat-affected zone, which means there are no thermal changes in the material and no heat-related distortion. The process enables tight tolerances and produces smooth, burr-free edges that often require no additional finishing. This saves time and reduces secondary processing costs.
Efficiency
Minimal material waste
Waterjet cutting creates minimal material waste thanks to efficient nesting and a narrow cutting kerf. Common cutting lines can also be used. The narrow kerf width enables accurate cutting and even complex details, improving the accuracy and quality of the final product.
Waterjet cutting also offers several options for production without the need for continuous operator presence.
Speed
Finish the job in one process
Additional finishing is usually not required, as the part is often ready directly from the waterjet cutting table.
Cutting can also be carried out with multiple cutting heads, and materials can be stacked on top of each other, which can multiply production speed.
Simplicity
Let’s make it easy
Waterjet cutting requires only water, electricity and, depending on the application, waterjet abrasive.
Fequentky asked questions
TamCut questions, answered
We have collected the questions customers ask us most often, together with the answers our own waterjet specialists give. The figures come from real cutting work with TamCut, not from theoretical maximums, so treat them as realistic starting points rather than guarantees — cutting speed, edge quality and taper always depend on the material, thickness and the quality you need.
1. Cutting and performance
TamCut can cut a wide range of materials using either pure water or abrasive waterjet cutting.
Typical materials include:
- stainless steel and structural steel
- aluminium, brass and copper
- titanium and special alloys
- glass and ceramic tiles
- stone and quartz composite
- carbon fibre and other composites
- plastics
- rubber and gasket materials
- foams
- plywood, wood and cardboard.
The suitable cutting method, speed and maximum material thickness depend on the material and the required cutting quality.
There is no single maximum thickness that applies to every material.
Practical cutting capacity depends on factors such as:
- the material
- the required cutting quality
- the acceptable taper
- the cutting speed
- the part geometry.
TamCut has successfully cut, for example, approximately 25-30 mm stainless steel, 40 mm aluminium, 25 mm carbon fibre composite and soft materials with a thickness of almost 50 mm.
Thicker materials can be cut, but the cutting speed decreases and taper increases.
Cutting speed depends on the material, thickness and required edge quality.
Examples of practical cutting speeds:
- 3 mm aluminium: approximately 500–700 mm/min
- 3 mm stainless steel: approximately 200–300 mm/min
- 5 mm stainless steel: approximately 80–180 mm/min
- 3 mm carbon fibre: up to 1300 mm/min
- 3 mm plywood with pure water cutting: up to 1300 mm/min
- 3 mm glass: approximately 510 mm/min
- 10 mm ceramic tile: approximately 250 mm/min.
The actual speed is always selected according to the material and the required quality.
Waterjet cutting produces a cold-cut edge without a heat-affected zone.
Cut quality is particularly affected by:
- material thickness
- cutting speed
- nozzle condition
- abrasive quality
- the selected cutting parameters.
Slower cutting generally produces a smoother and straighter edge. Faster cutting increases productivity, but may also increase striation and taper.
No.
Waterjet cutting is a cold cutting process. It does not normally cause thermal distortion, melting, discolouration or hardening of the cut edge.
This is particularly beneficial for metals, composites, plastics and research samples where the original material properties must remain unchanged.
All conventional waterjet cutting produces some degree of taper, especially when cutting thick materials at higher speeds.
TamCut does not have active taper compensation. Taper can nevertheless be reduced by:
reducing the cutting speed
optimising the cutting parameters
using a nozzle in good condition
selecting the appropriate abrasive
ensuring correct alignment of the cutting head.
For tolerance-critical applications, we always recommend a sample cut using the customer’s own material.
Yes.
TamCut supports both pure water and abrasive waterjet cutting.
Pure water cutting is suitable for materials such as:
- rubber
- foam
- gasket materials
- thin plywood
- cardboard
- other soft materials.
Abrasive cutting is used for harder materials such as metals, glass, stone, ceramics and composites.
Yes.
A sample cut is the best way to verify:
- a suitable cutting speed
- cut quality
- taper
- piercing behaviour
- material suitability
- a realistic cycle time.
The customer can send their own material and desired geometry to Muototerä for evaluation.
2. Software and workflow
TamCut works with external CAD/CAM software that converts the customer’s geometry into a cutting program for the machine.
The software is available either as a purchased licence or as a subscription. Depending on the selected licence, the software may include:
- Automatic and manual nesting
- Material and cutting parameter databases
- Toolpath generation
- Post-processing for TamCut
The most suitable software configuration is selected according to the customer’s applications and production needs.
TamCut includes the machine control and HMI required to operate the waterjet cutting machine.
CAD/CAM software is supplied separately as either a purchased licence or a subscription. This allows the software package to be selected according to the customer’s required file formats, nesting functions and production workflow.
CAD/CAM training can be provided remotely.
The supported file formats depend on the selected CAD/CAM software package.
Common two-dimensional CAD formats can be converted into TamCut cutting programs. More advanced software packages support a wide range of CAD formats, nesting, material databases and automatic toolpath generation.
For a specific file format, please contact Muototerä.
Yes.
The TamCut HMI is mirrored to an industrial PC, providing a clear and familiar interface for machine operation. The PC is not part of the machine’s safety control system and can therefore be replaced relatively easily if required.
An internet connection is not required for normal machine operation.
3. Installation and utilities
The recommended installation footprint includes the machine and the space required for normal operation and access.
- TamCut 400: approximately 1.5 × 2.4 metres
- TamCut 1000: approximately 1.5 × 3.0 metres
Additional space may be required depending on the room layout, material handling and local safety requirements.
TamCut is designed for straightforward installation.
The main requirements are:
- 400 V, 16 A three-phase electrical connection
- Clean water supply
- Drain connection
- Level and sufficiently strong floor
- Suitable space for operation and maintenance
After unpacking, the machine is connected to the water supply, drain and electrical outlet.
The exact installation requirements are provided before delivery.
No.
TamCut does not require a compressed-air connection for normal operation.
The high-pressure water flow is approximately 1.2 litres per minute with the standard nozzle configuration.
The water supply should provide sufficient flow and stable inlet pressure for reliable operation. Clean inlet water and suitable filtration are important for pump and nozzle life.
Water is not recirculated through the cutting process.
Clean inlet water is important for the reliability and service life of the high-pressure system.
Muototerä recommends:
- Approximately 20 µm inlet filtration
- Assessment of local water hardness
- Anti-scale treatment when required
The appropriate water treatment depends on the local water quality.
TamCut is designed for quick commissioning when all required connections have been prepared in advance.
The main installation steps are:
- Unpacking and positioning the machine
- Connecting the drain
- Connecting the inlet water
- Connecting the 400 V electrical supply
- Performing the initial checks and commissioning
Installation time depends on site readiness and the selected delivery package.
Yes.
Every TamCut machine includes one day of operator training at Muototerä in Tampere, Finland.
For the most effective training, the recommended group size is a maximum of three participants.
On-site training and commissioning at the customer’s premises are available as additional services. CAD/CAM training can also be provided remotely.
4. Noise and working environment
The sound level depends on the material, cutting method and whether cutting takes place above or below the water surface.
The sound level is below 80 dB under normal operating conditions.
Cutting below the water surface generally reduces noise compared with cutting above the water surface. The enclosed cabinet also helps contain cutting noise, spray and abrasive.
Yes.
Depending on the material and application, cutting can be performed below the water surface. Underwater cutting can reduce noise, splash and the amount of airborne mist.
5. Abrasive system
TamCut can use either 80 mesh or 120 mesh garnet abrasive.
For the standard TamCut nozzle configuration, 120 mesh abrasive is recommended. Its finer grain size works well with the compact focusing tube and helps provide stable abrasive flow and good cutting performance.
The standard abrasive feed rate is approximately 300 grams per minute during abrasive cutting.
Actual abrasive consumption depends on the amount of active cutting time. Abrasive is not consumed during positioning movements or when pure water cutting is used.
The abrasive container has a capacity of approximately 18 litres.
With the standard abrasive feed rate, one full container provides approximately one hour of continuous abrasive cutting.
The container can be refilled while the machine is cutting, allowing longer jobs to continue without interruption.
The standard abrasive system supplies a fixed abrasive flow of approximately 300 grams per minute.
Automatic abrasive flow monitoring is not included. The operator should check the abrasive level and ensure that abrasive is flowing correctly during cutting.
6. Piercing and sensitive materials
Yes.
TamCut can pierce most suitable materials directly with the waterjet before starting the cutting path.
Piercing behaviour depends on the material, thickness and risk of cracking or delamination.
Yes.
TamCut includes low-pressure piercing for materials that benefit from a gentler starting process. This is especially useful for materials such as:
- Glass
- Laminates
- Carbon fibre composites
Brittle materials
- Materials that may delaminate during full-pressure piercing
Piercing parameters should be selected according to the material and thickness.
Yes.
A cutting path can be programmed to start from an existing hole when this is preferable for the material or component.
TamCut does not include a separate drilling spindle. Any required mechanical starting hole must therefore be made before placing the workpiece in the machine.
7. Maintenance and consumables
Typical service life under suitable operating conditions is approximately:
- Water orifice: 40–50 operating hours
- Focusing tube: 40–60 operating hours
Actual service life depends on:
- Water quality
- Abrasive quality
- Alignment of the cutting head
- Operating pressure
- Piercing frequency
- Correct installation
- Material and cutting conditions
The components should be inspected if cutting quality, jet stability or cutting performance changes.
The first scheduled pump maintenance is performed at approximately 300 operating hours or after one year.
Depending on water quality, operating conditions and pump condition, components may remain operational for considerably longer. However, the specified inspection and maintenance intervals should be followed to ensure reliable operation and to identify wear before it causes unplanned downtime.
Abrasive and removed material accumulate in the cutting tank during operation.
The standard machine uses manual tank cleaning. The water and abrasive sludge are removed by the operator as part of normal maintenance.
TamCut does not recirculate cutting water or abrasive.
Cleaning frequency depends on operating hours, materials and the amount of abrasive cutting performed.
No. Cutting water is discharged to the prepared drain connection, and used abrasive accumulates in the cutting tank for manual removal.
Local requirements for wastewater and sludge disposal must be followed, particularly when cutting materials that may contain hazardous substances.
8. Warranty and support
TamCut is supplied with a warranty of 12 months or 300 operating hours, whichever occurs first.
The detailed warranty conditions, exclusions and responsibilities are specified in the commercial offer and delivery documentation.
Consumables and parts subject to normal wear are not covered by the warranty.
Muototerä provides:
- Technical telephone and remote support
- Spare and wear parts
- Preventive maintenance
- Troubleshooting
- Pump maintenance
- Operator training
- CAD/CAM assistance
- On-site service when required
Support and spare parts are provided from Tampere, Finland.
9. Safety and compliance
TamCut is designed as an enclosed waterjet cutting machine, with the cutting process and high-pressure components protected inside the machine cabinet.
Key safety features include:
- The machine cannot perform cutting movements while the protective cover is open
- High-pressure water is automatically disabled when access to the cutting area is opened
- The cutting head, waterjet and abrasive remain inside the enclosed cutting area
- High-pressure pipes and connections are routed inside the machine structure and protected from accidental contact
- The enclosure contains water spray, abrasive and fragments generated during cutting
- Emergency stop functions are provided for immediate machine shutdown
- Safety-related functions are monitored by the machine control system with industrial safety grade
These features prevent the operator from accessing the moving cutting head or high-pressure waterjet during normal operation.
Operators must still follow the instructions in the user manual, use suitable personal protective equipment during maintenance and never bypass the machine’s safety devices.
Yes.
TamCut is designed and manufactured in accordance with the applicable European machinery, electrical safety and electromagnetic compatibility requirements.
The machinery complies with:
- Machinery Directive 2006/42/EC
- Electromagnetic Compatibility Directive 2014/30/EU
- Low Voltage Directive 2014/35/EU
Applied standards include:
- EN ISO 12100 – Risk assessment and risk reduction
- EN ISO 13850 – Emergency stop function
- EN 60204-1 – Electrical equipment of machines
- EN ISO 13849-1 – Safety-related parts of control systems
- EN 61000-6-2 – Electromagnetic immunity for industrial environments
- EN ISO 14120 – Guards and protective devices
An EC Declaration of Conformity and the required technical documentation are supplied with the machine.
Contact us
Ready to bring waterjet cutting into your application?
Talk to our team and find out whether TamCut fits your materials, parts and production needs.